Explore our top-tier heavy-duty industrial racking and modular storage engineering systems optimized for global freight distribution and high-density warehouse deployment.
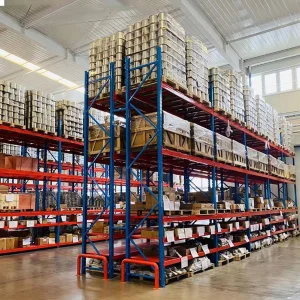
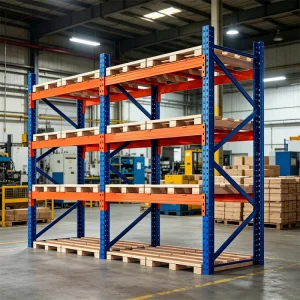
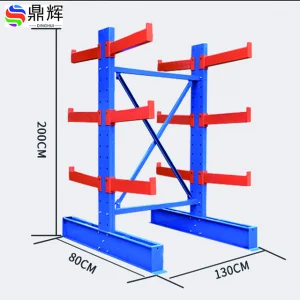
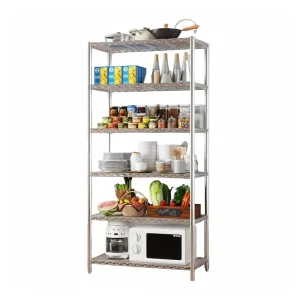
Foshan Dinghui Intelligent Warehousing Technology Co., Ltd. combines premier industrial manufacturing with robust global logistics coordination to deliver seamless cross-border supply chain solutions.
Foshan Dinghui Intelligent Warehousing Technology Co., Ltd., established in 2015, is a leading manufacturer specializing in heavy-duty industrial storage racks, pallet racking systems, and automated warehouse solutions. Spanning a modern manufacturing base of 38,000 square meters, we bring together 12 years of industry experience and 8 years of direct global export expertise, generating an annual export revenue of over $25 million USD.
Equipped with advanced automated roll-forming and powder-coating production lines, our quality control procedures adhere to rigorous ISO 9001 and CE certification standards. We implement comprehensive product testing protocols, including raw material tensile testing, structural load-bearing simulation, powder coating adhesion tests, and weld non-destructive inspection (NDI). Supported by a dedicated 35-member QA/QC team, we ensure that every racking component strictly meets international safety and durability standards.
Operating with a strong international OEM/ODM trade background, our primary markets span North America, Europe, Southeast Asia, and the Middle East. Backed by a robust network of over 850 reliable supply chain partners, we serve a diverse global client base, including 3PL logistics providers, industrial warehouse operators, e-commerce fulfillment centers, and regional distributors.
Innovation and custom engineering drive our success. Supported by 18 experienced senior R&D engineers, we offer extensive OEM/ODM customization options, including tailored load capacities, custom dimensions, seismic-resistant structural design, special powder-coating finishes, and automated system integration. Driven by continuous technical improvement, we successfully launched 45 new product designs and structural upgrades last year, empowering our global partners to optimize their warehouse efficiency.
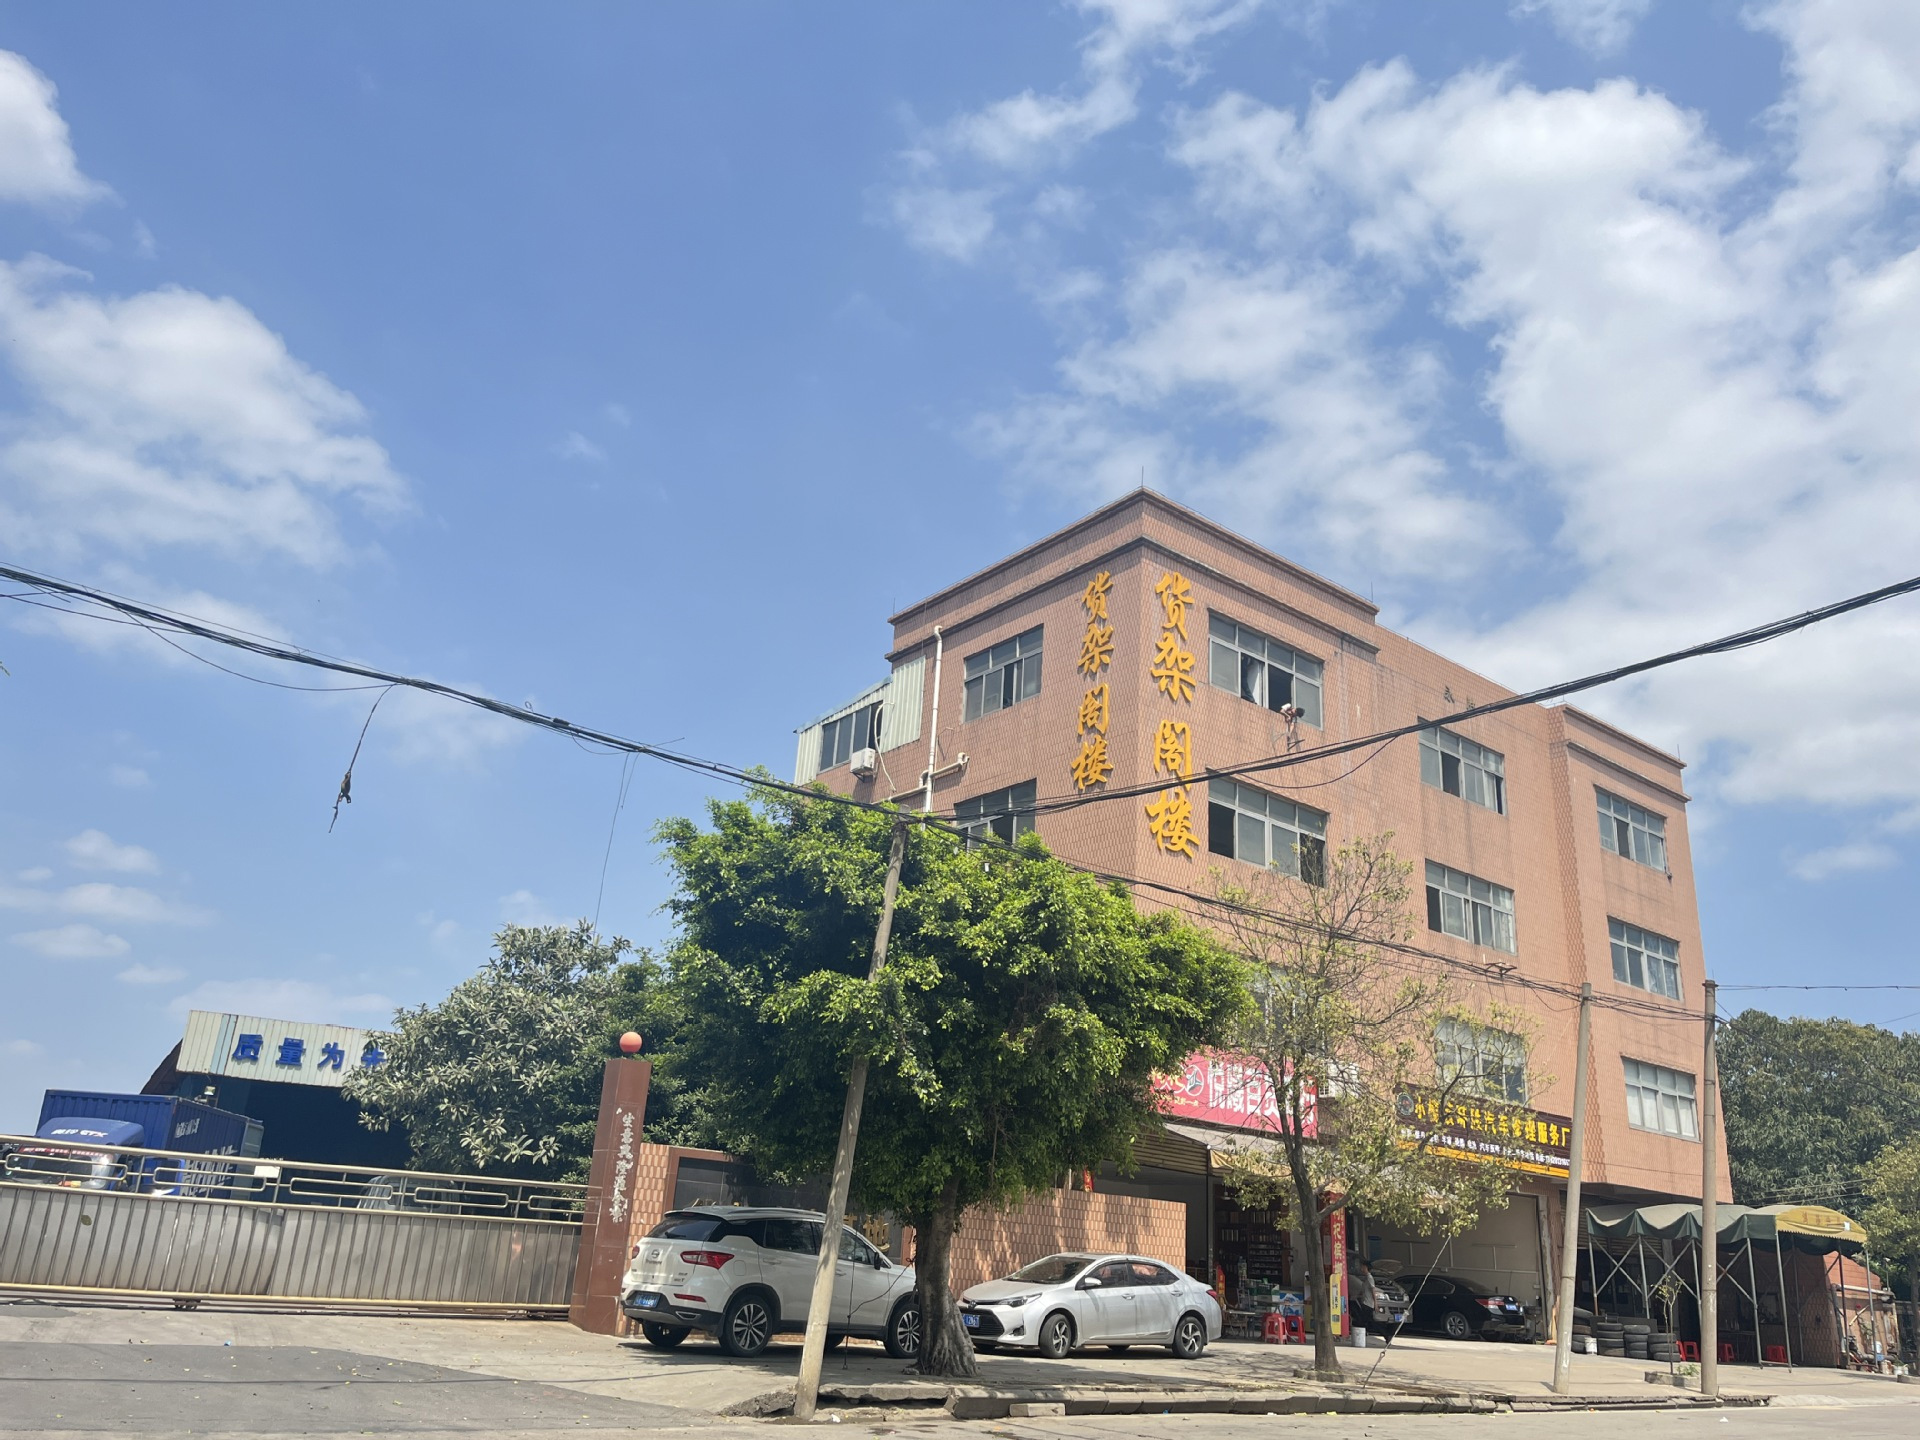
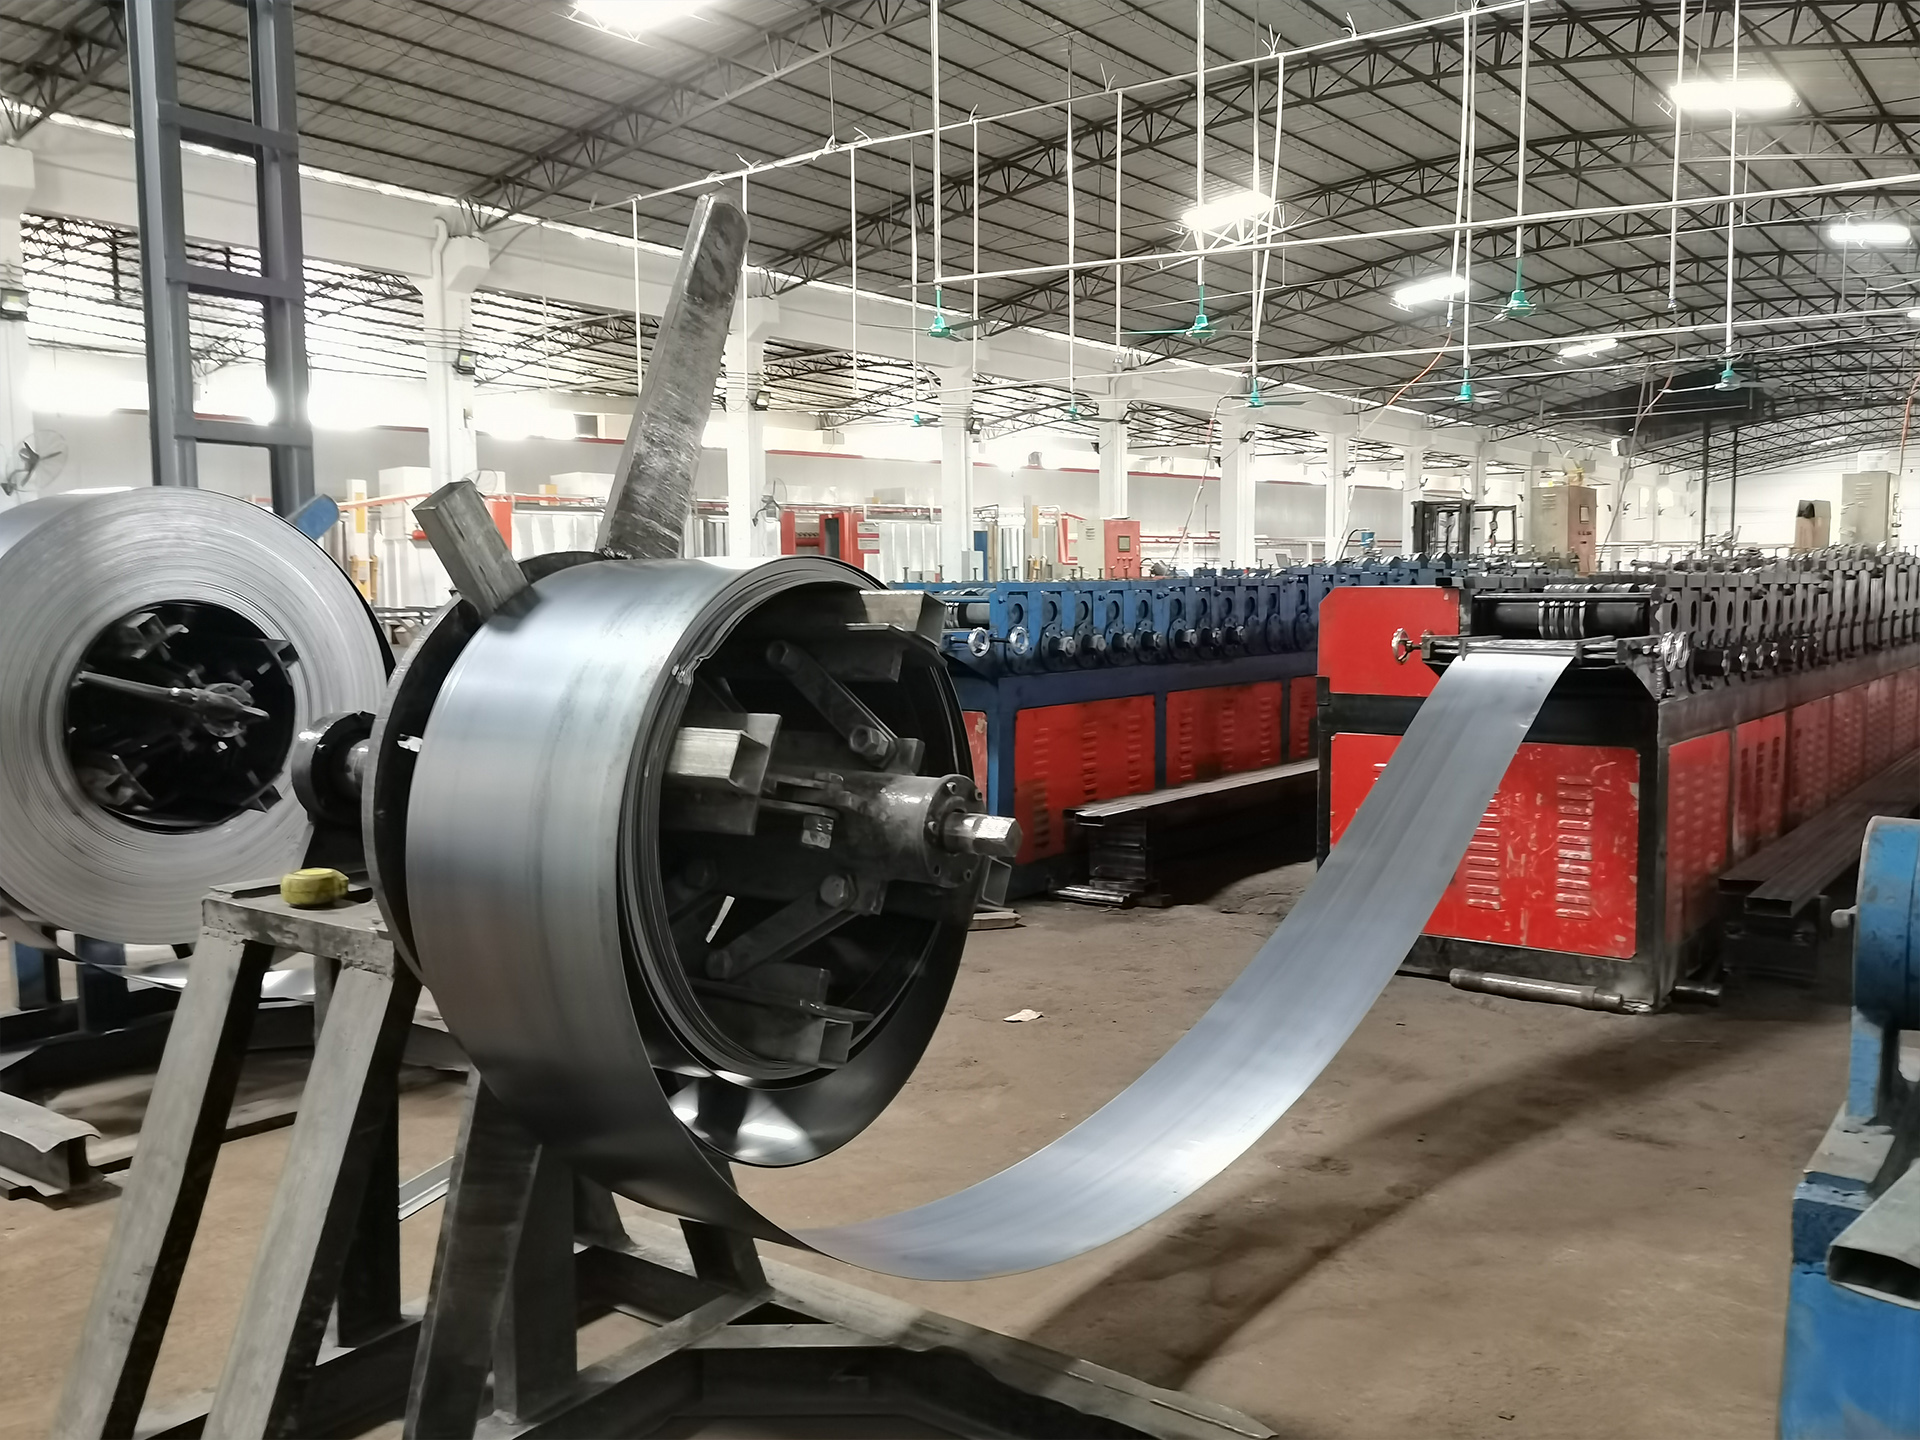
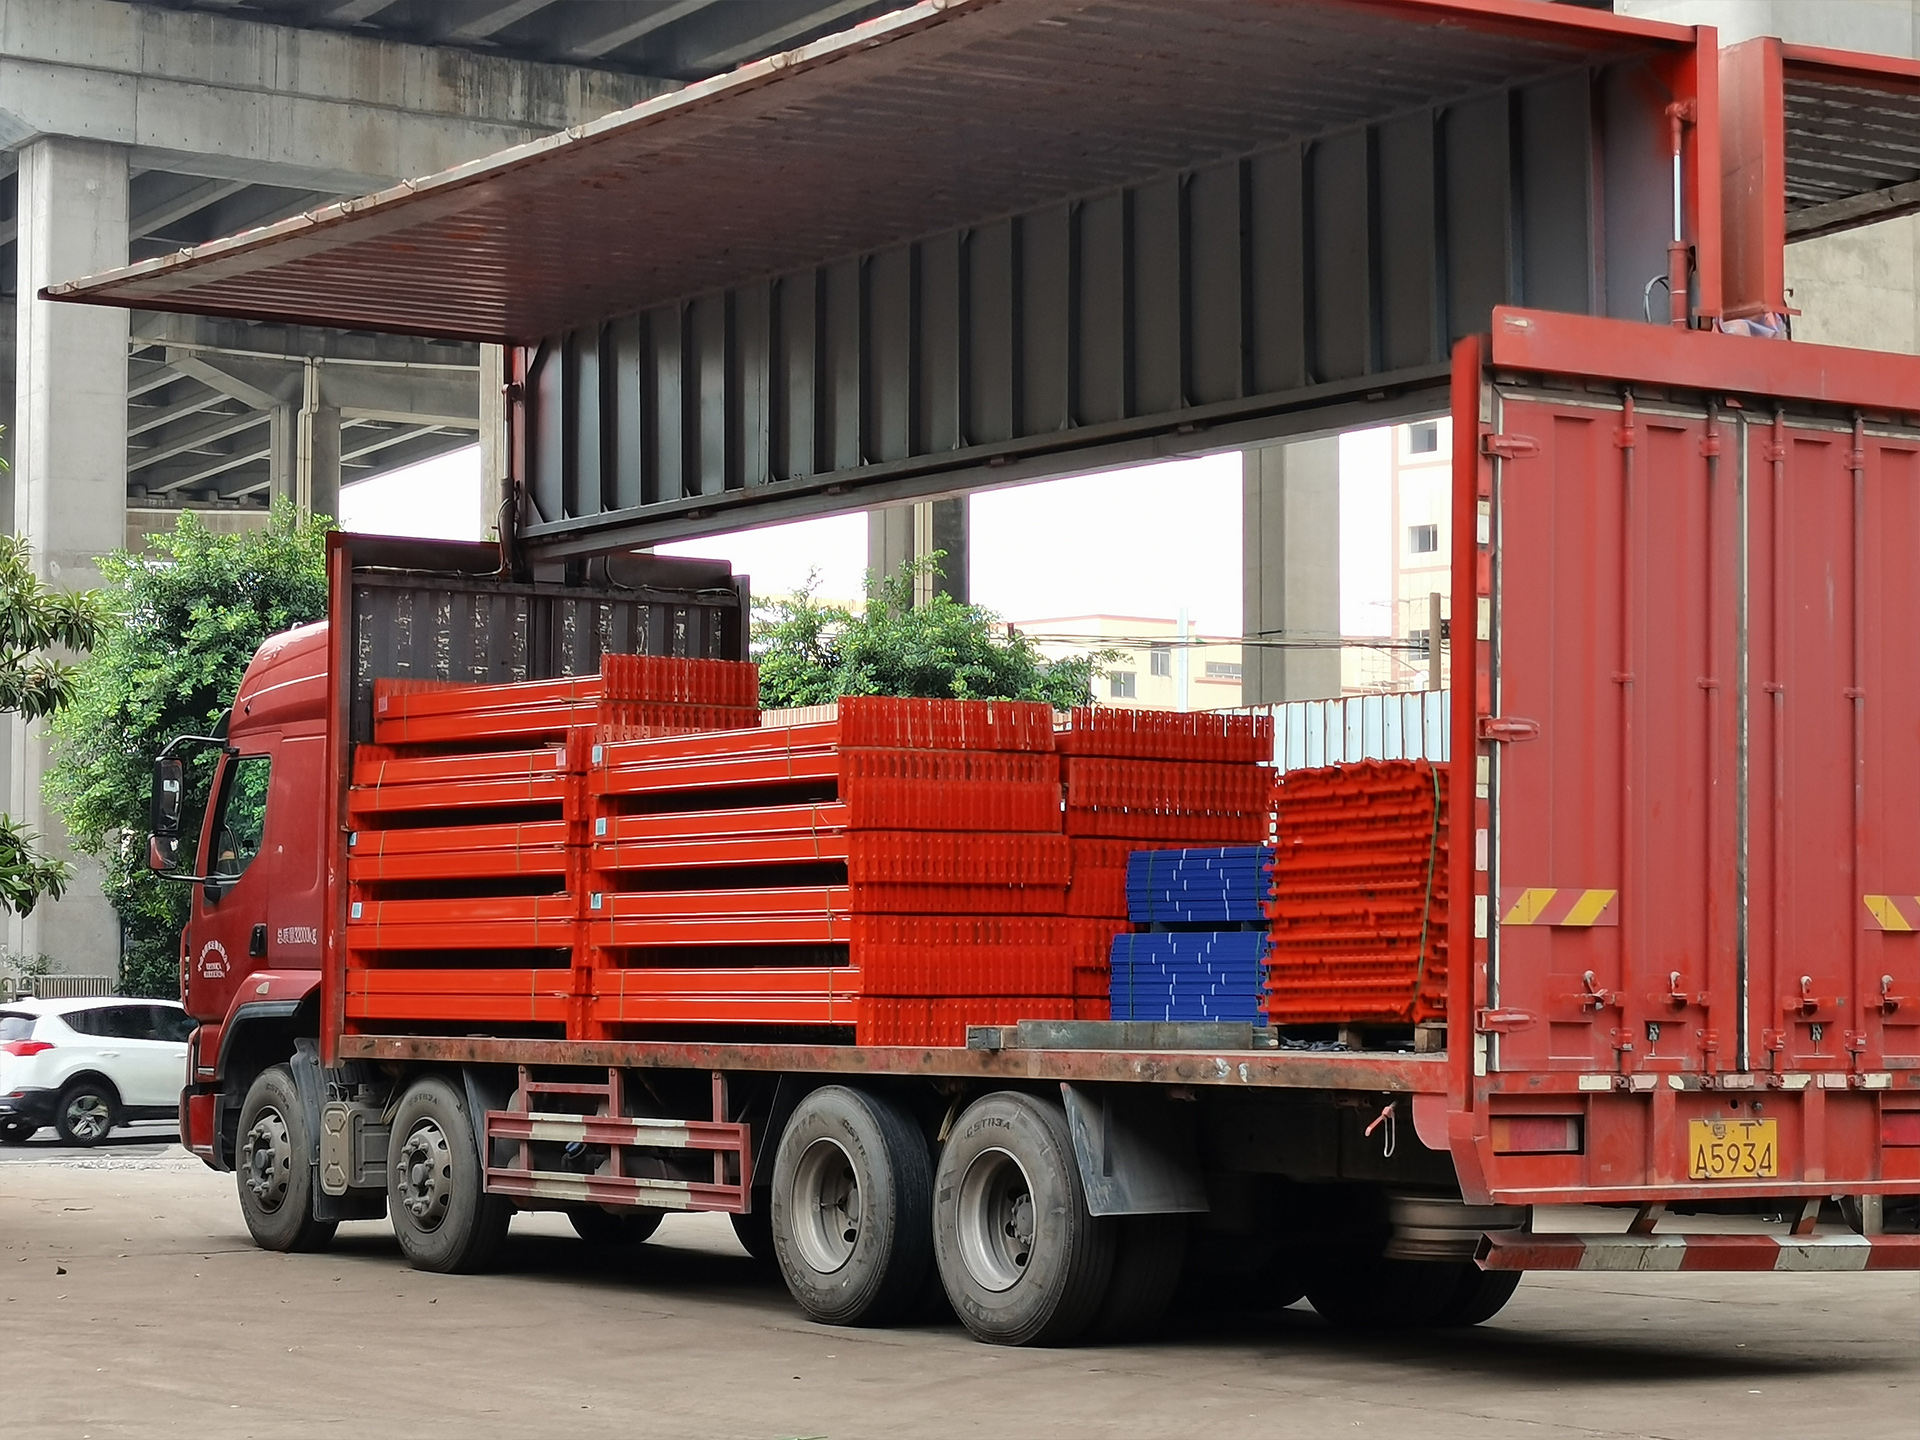
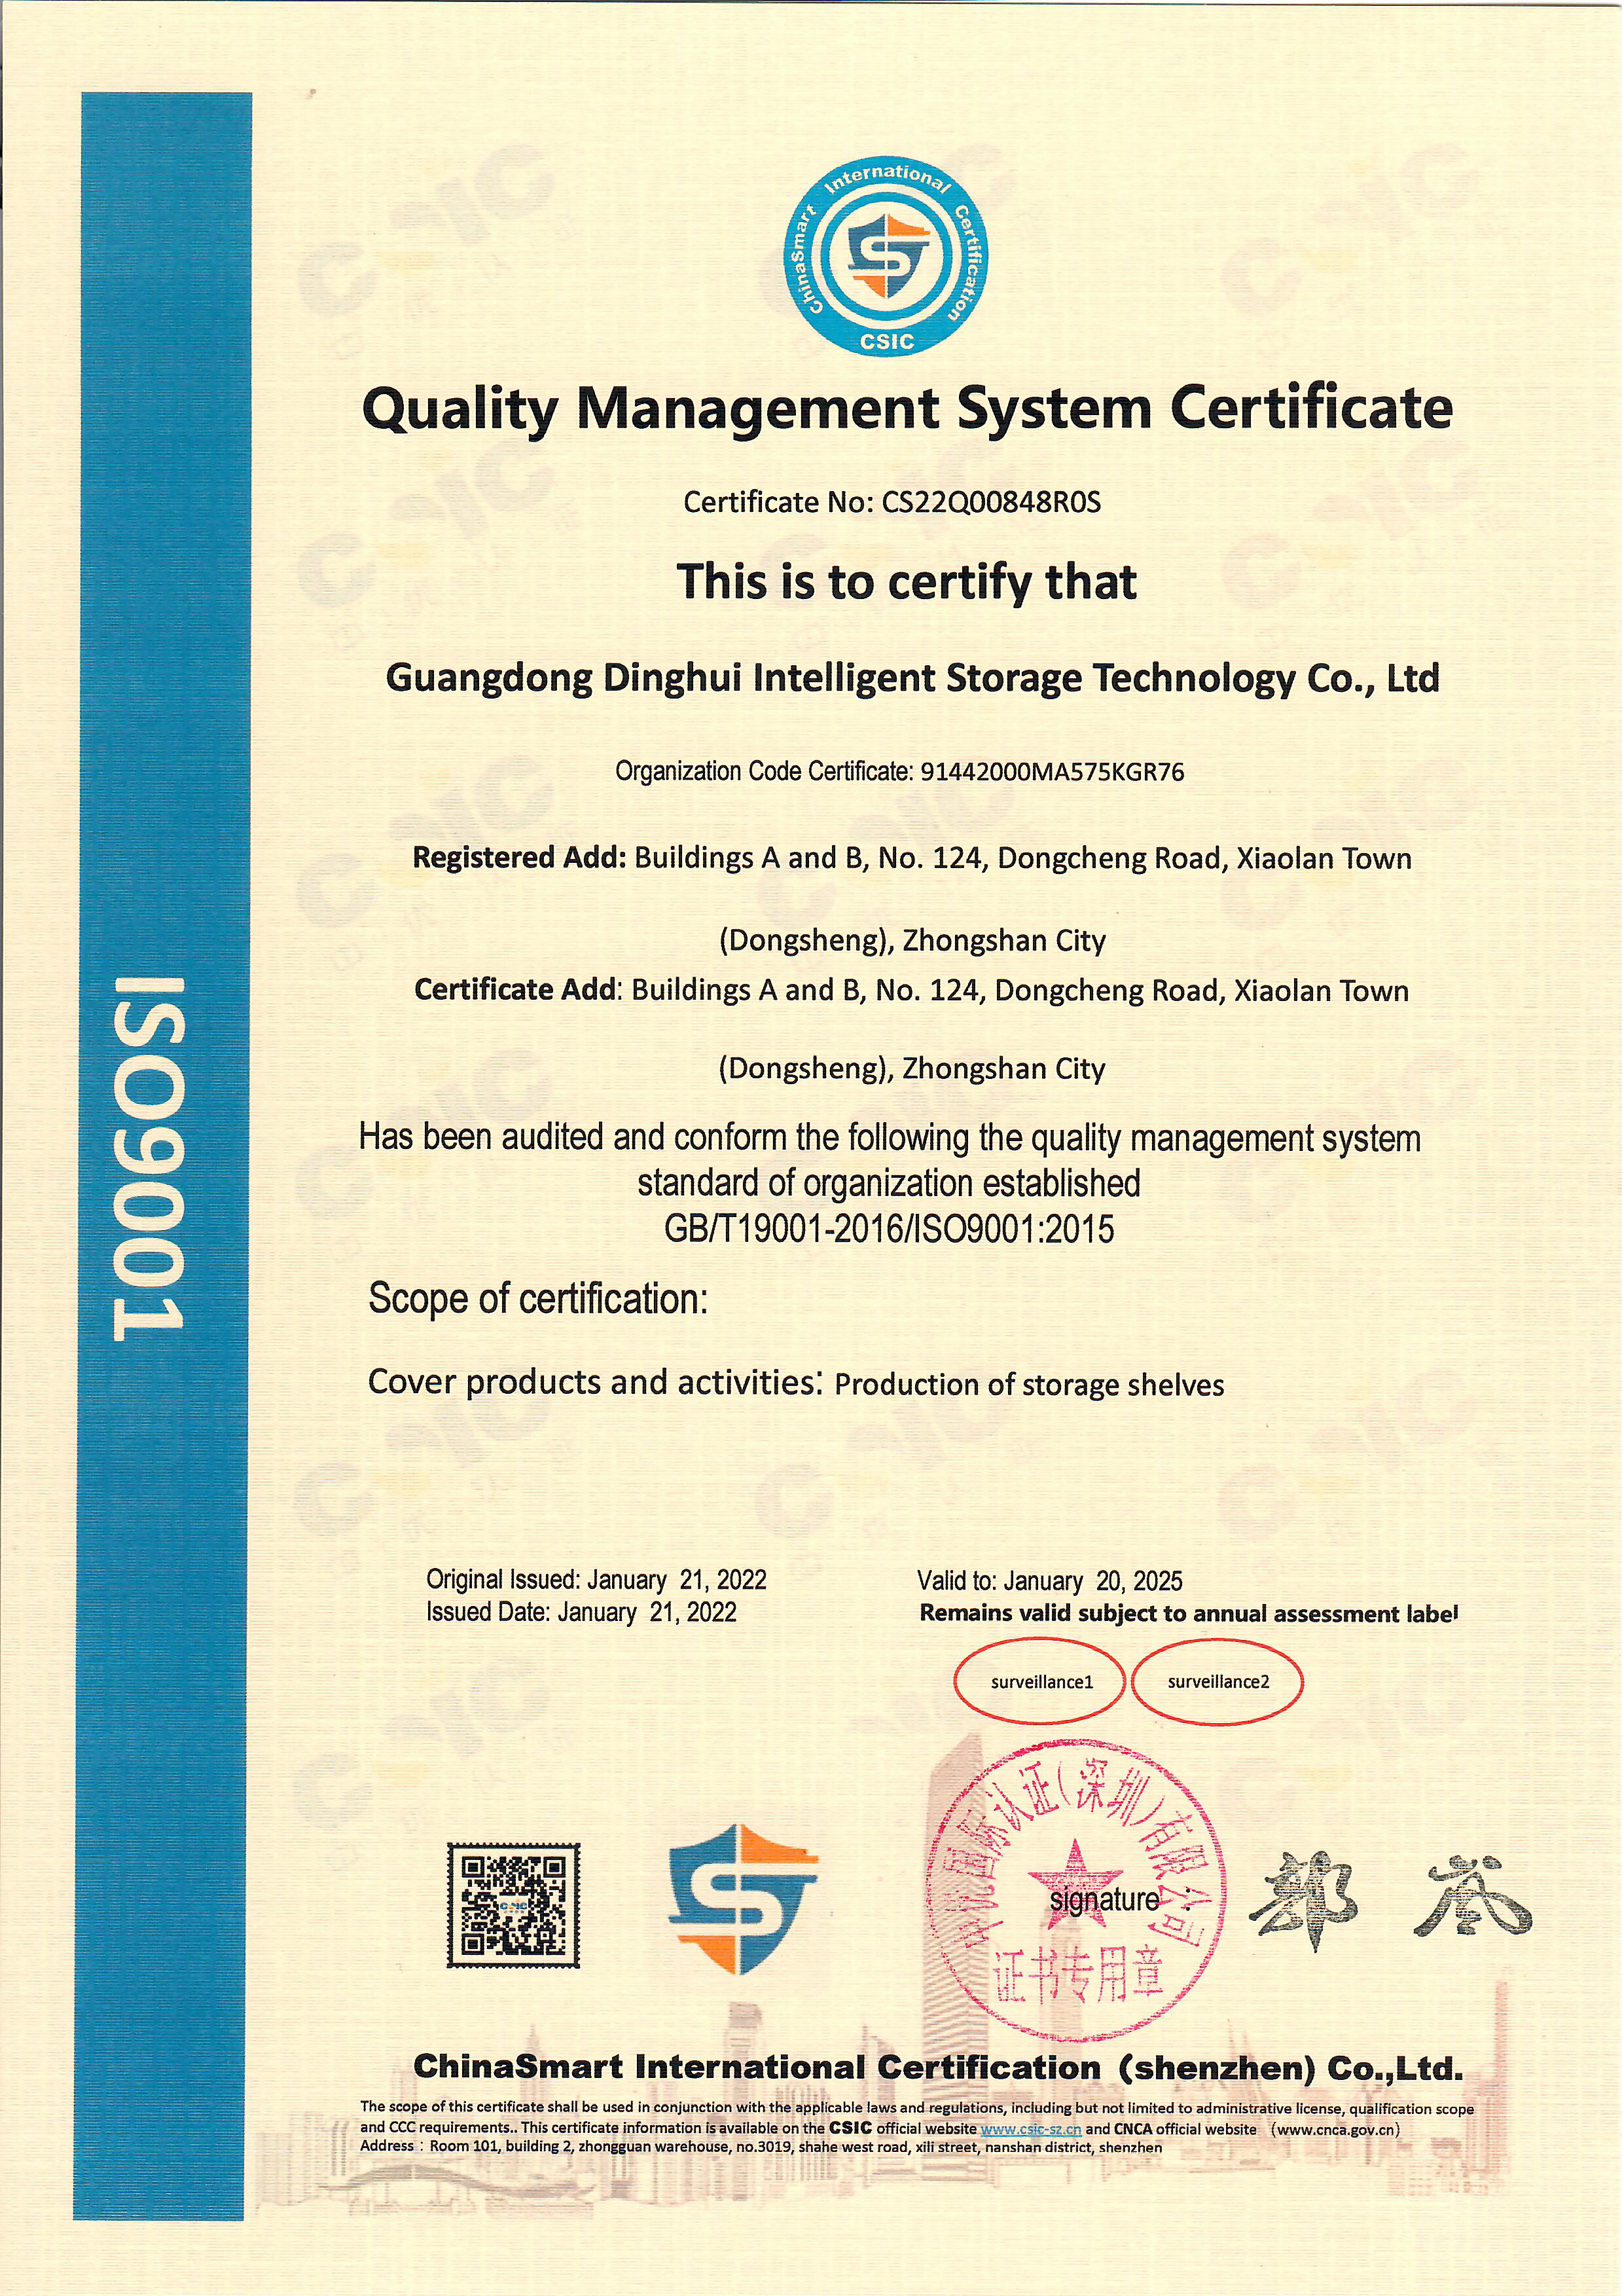
Demonstrating verified operational scale, robust manufacturing capacity, and established global distribution capability.
Strategic analysis of cross-border trade dynamics, localized application scenarios, and future technological roadmaps in industrial logistics.
The global freight forwarding and industrial storage sector is undergoing a massive digital and structural transformation. Driven by surging e-commerce demands and regional supply chain diversification, businesses require highly durable, modular storage systems integrated with agile international shipping logistics to minimize lead times and warehouse overhead.
From automated fulfillment centers in North America to high-density distribution hubs across Europe and Southeast Asia, our heavy-duty racking solutions are engineered to withstand diverse environmental conditions, seismic requirements, and intensive daily operations, ensuring maximum cube utilization.
Integrating IoT sensors, automated guided vehicles (AGVs), and smart inventory tracking into physical steel storage frameworks represents the future of warehousing. Dinghui continuously invests in advanced R&D to bridge heavy manufacturing with smart logistics ecosystems.
Expert answers regarding our manufacturing capabilities, quality assurance protocols, and global freight forwarding partnerships.
We combine direct factory manufacturing across 38,000 square meters with robust international export expertise. Our seamless coordination with over 850 supply chain partners ensures secure packaging, optimized container loading, and reliable global freight delivery.
All products adhere to ISO 9001 and CE standards. Our 35-member QA/QC team conducts rigorous tensile testing, load-bearing simulations, powder-coating adhesion checks, and weld inspections before dispatch.
Yes. Supported by 18 senior R&D engineers, we provide tailored load capacities, custom dimensions, seismic engineering designs, and specialized finishes tailored to your exact warehouse specifications.
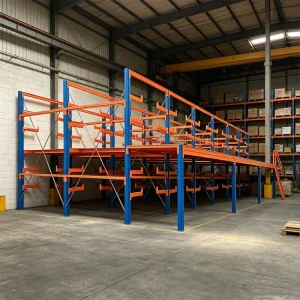
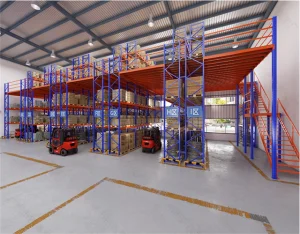
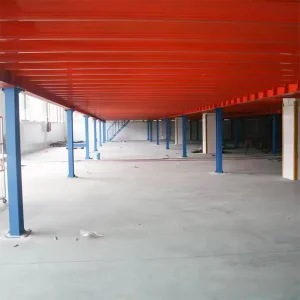
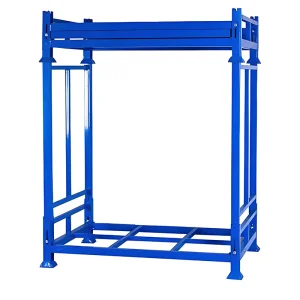
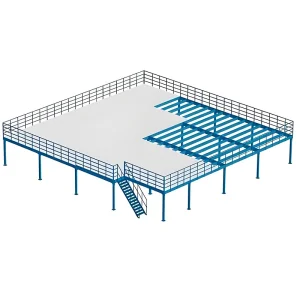
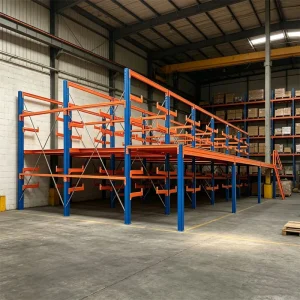
Browse our extended catalog of high-performance industrial shelving, mezzanine floors, and heavy-duty storage systems.
 Dinghui Racking