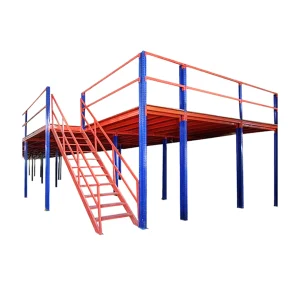
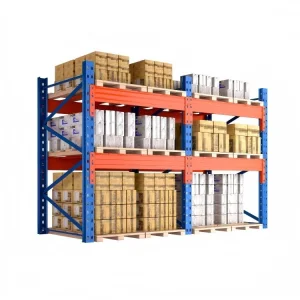
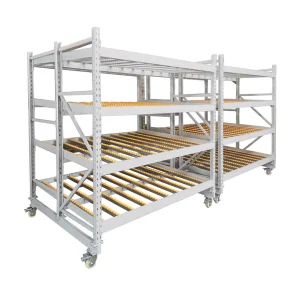
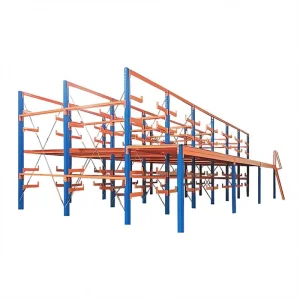
Foshan Dinghui Intelligent Warehousing Technology Co., Ltd. (est. 2015) is a pioneer in storage infrastructure. With 38,000 sqm of manufacturing space, we bridge the gap between heavy-duty engineering and smart logistics. Our 12 years of industry experience and $25M+ export volume reflect our authority in providing scalable, ISO-certified storage solutions. We don't just supply racks; we engineer the backbone of global supply chains.
The global packaging and storage materials market is shifting toward High-Density Automated Storage. Modern enterprises demand precision-engineered, corrosion-resistant, and modular systems that can adapt to changing SKU volumes. Our R&D team continuously integrates seismic-resistant designs and smart modularity to meet the rigorous demands of North American and European logistics hubs.
Our roadmap focuses on "Digital Warehouse Twin" integration. By utilizing high-tensile cold-rolled steel and advanced non-destructive inspection (NDI) protocols, we ensure our components last 30% longer than market averages. The future of packaging and material handling is intelligent—we are currently piloting IoT-enabled shelving that tracks inventory weight in real-time.
We leverage 18 senior R&D engineers to provide fully customized load-bearing solutions tailored to your specific warehouse footprint.
We strictly adhere to ISO 9001 and CE standards, verified by 35 dedicated QA/QC professionals.
With 8 years of export expertise, we have successfully deployed solutions in 40+ countries with localized installation support.
 Dinghui Racking